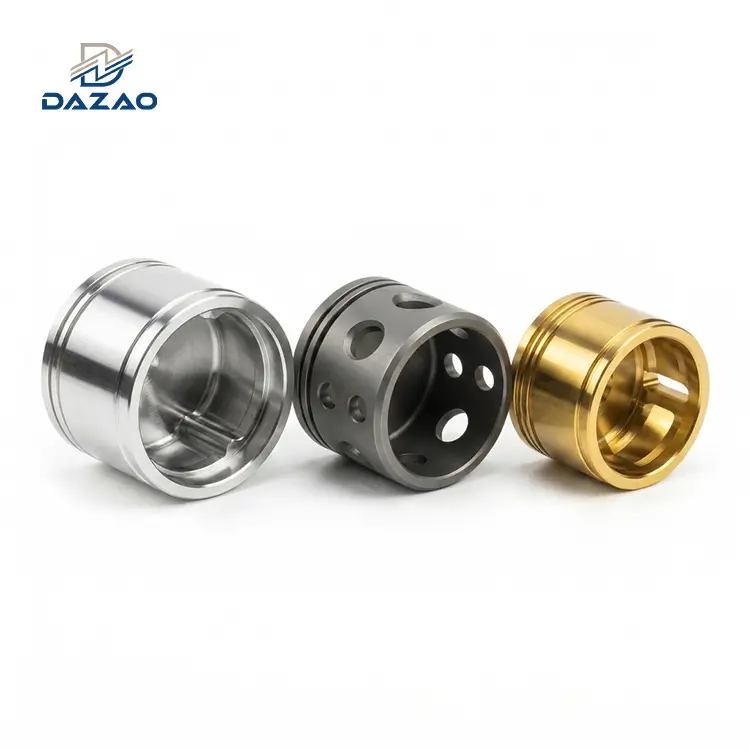

Hole features account for 30% to 50% of total cycle time in precision machining and over 60% of shop-floor scrap. Economical hole production requires matching hole geometry to standard rotary tooling. Keep depth-to-diameter ratios below 5:1, avoid modeled flat bottoms on blind holes without functional necessity, calculate pilot depths to account for 118° or 135° drill points and tap lead-ins, and assign tolerances based on manufacturing process thresholds (Drilling: ±0.1 mm / IT11 to IT13; Reaming: ±0.01 mm / IT7 to IT8; Boring: ±0.005 mm / IT6 to IT7).
The True Cost of Hole Making in Precision CNC Machining
In precision subcontract manufacturing, hole fabrication represents the highest concentration of tool wear, chip evacuation failure, and dimensional variance on the machining floor. While modern CAD software allows an engineer to place a 3.15 mm diameter hole with an 80 mm depth and a flat bottom in seconds, manufacturing that geometry requires specific tool paths, specialized tooling, feed derating, and secondary operations that multiply unit piece price. The total production cost of a hole is governed by the cumulative sum of tooling wear, machine cycle time, coordinate metrology overhead, and part scrap risk.
Following standardized CNC hole design guidelines directly controls part piece price. A circular hole is not a static 2D drawing callout; it is the physical negative volume generated by a rotating cutting tool operating under heavy axial thrust and radial deflection forces. At Dazao, our production data across aerospace housings, automotive powertrain components, and medical manifolds demonstrates that unoptimized hole geometries cause the majority of on-machine tool failures and scrapped parts within our custom precision CNC machining services.

When specifying CNC hole diameter and depth, design choices dictate four mechanical factors on the shop floor:
· Tooling Availability: Standard off-the-shelf tooling vs. custom ground carbide drills requiring extended procurement lead times.
· Kinematic Rigidity: Tool overhang length versus diameter, governing cantilever deflection and vibration harmonics.
· Chip Evacuation Dynamics: The ability of cutting fluid at 20 to 70 bar (300 to 1000 psi) to flush chips out of the flutes before chip packing breaks the tool.
· Metrology Complexity: Standard plug gauges vs. air gauges vs. coordinate measuring machine (CMM) stylus access limits.
Critical DFM Blind Spots: CAD Modeling Traps, Hydraulic Lock & Surface Finish Risks
Generic design handbooks list standard hole sizes, but production scrap typically originates from three specific failure modes observed during manufacturing operations.

CAD Conical Point Geometry vs. Usable Thread Depth Clashes
Modern parametric CAD tools default to cylindrical cuts that terminate in flat bottoms unless the designer manually specifies a conical tip. In production, standard solid carbide and high-speed steel (HSS) twist drills are ground with either a 118° point angle for general purpose mild steels or a 135° split point for stainless steels, titanium alloys, and high-nickel superalloys. Geometrically, the axial height of a 118° drill cone adds approximately 0.300 times the drill diameter to the total depth, while a 135° split point adds approximately 0.207 times the diameter.
When an engineer designs a flat-bottom CNC blind hole design, the machine operator cannot finish the hole with a single drilling cycle. The shop must execute a primary drilling operation followed by a secondary plunging operation using an end mill or flat-bottom drill. This secondary pass introduces tool deflection, creates chatter marks, and complicates internal geometries. Engineers can review how internal corner radii and bottom fillet cost impacts escalate total machining time during cavity clearing passes.
To establish safe clearance for blind tapped holes, the total pilot hole depth must equal the required functional thread depth, plus an extra safety allowance of 3 to 5 thread pitches, plus the axial depth of the drill point cone. The issue intensifies with threaded blind holes because standard spiral-flute taps feature a lead chamfer of 2 to 3 imperfect threads. If a drawing specifies 15 mm of full thread depth inside an 18 mm deep drilled pilot hole, the tap impacts the bottom conical face before reaching depth, leading to catastrophic tap breakage inside the workpiece.
Hydraulic Lock & Thin-Wall Hoop Stress Distortion
In precision components with thin surrounding structures, high-speed tapping and reaming operations inside blind holes create an enclosed fluid compression zone. As a tool enters a blind hole with cutting fluid delivered at 30 liters per minute, the fluid and trapped air cannot escape through the restricted flute clearances, generating severe internal pressure.
According to thin-walled pressure vessel mechanics, the resulting internal hoop stress equals the dynamic fluid pressure multiplied by the hole radius, divided by the surrounding wall thickness. When this internal stress exceeds the material yield strength (such as 276 MPa for Al6061-T6 or 310 MPa for Brass C36000), the surrounding wall undergoes permanent outward plastic deformation. Post-machining CMM inspections reveal outward wall bulging of 0.02 mm to 0.05 mm and cylindrical runout errors on the outer profile. Engineers should cross-reference our minimum CNC wall thickness engineering rules to prevent structural distortion under high cutting pressures.
To safeguard thin-walled blind holes during manufacturing:
· Maintain a minimum surrounding wall thickness of at least half the hole diameter for structural integrity during high-pressure fluid-cooled cutting.
· When a wall thickness below 1.0 mm is unavoidable, utilize thread milling instead of tapping, derate coolant delivery pressure, or add an external pressure relief micro-channel to the CAD model.
Chemical Entrapment & Post-Anodizing Acid Bleed-Out
Blind holes with high depth-to-diameter ratios exceeding 5:1 trap chemical solutions during surface finishing treatments, including sulfuric acid anodizing (MIL-A-8625), electroless nickel plating (AMS-2404), and chemical conversion coatings (MIL-DTL-5541).
Due to liquid surface tension and blind micro-pockets, standard post-plating deionized water immersion rinses fail to flush trapped acid out of the hole base. During thermal curing, baking, or storage:
· Trapped acid heats up, expands, and weeps out of the hole entrance (acid bleed-out).
· The weeping acid destroys the surrounding anodized layer, leaving white, chalky aluminum oxide or degraded plating margins.
· Plating solutions fail to circulate inside blind micro-holes with diameters under 2.0 mm, creating unplated raw metal zones that corrode during salt spray testing (ASTM B117).
Design Mitigation Guideline: For parts requiring anodizing or plating, provide through-holes wherever possible. If blind geometries are mandatory, add a functional drain orifice of at least 1.5 mm diameter at the base or specify clear masking protocols on critical drawing faces.
Depth-to-Diameter (L/D) Limits & Deep Hole Tool Deflection Mechanics
Controlling hole manufacturing cost requires an understanding of how the CNC hole depth to diameter ratio changes cutting dynamics from basic shearing to deep-hole extraction.

Standard Hole Sizes for CNC Machining vs. Custom Diameter Tooling
Standardizing hole sizes allows machine shops to utilize off-the-shelf solid carbide drills with standard corner radii, coatings (AlTiN, TiSiN, DLC), and standard holder collets (ER, hydraulic, shrink-fit). Aligning hole geometry with standard hole sizes for CNC machining eliminates custom ground tool costs. Specifying non-standard diameters (such as 6.15 mm instead of 6.00 mm or 6.35 mm) forces the shop to step-bore the diameter, circular interpolate with smaller cutters, or purchase specialty tools. Reviewing our guide to structural aluminum machining cost drivers illustrates how non-standard tool callouts compound piece price.
Euler-Bernoulli Cantilever Deflection & Drill Wander Dynamics
As drill depth increases, the tool behaves as a cantilever beam subjected to combined axial compression thrust force and torsional moment. Under Euler-Bernoulli beam theory, the lateral deflection at the drill tip is directly proportional to the unbalanced radial cutting force multiplied by the cube of the tool overhang length, and inversely proportional to the material modulus of elasticity and the second moment of area.
Because the second moment of area scales with the fourth power of the tool diameter while deflection scales with the cube of the length, doubling the hole depth increases drill tip deflection eightfold. Conversely, reducing the drill diameter by half increases deflection sixteenfold. This geometric relationship governs tool selection across all hole-making operations.
Production Tier Matrix: Standard Drilling to Deep Gun Drilling
The table below defines manufacturing classifications and machine setup requirements when executing CNC deep hole drilling design across varying aspect ratios.
|
Depth-to-Diameter Ratio (L/D) |
Machining Classification |
Standard Production Process |
Required Machine Features |
Tolerance Capability (Diameter) |
True Position Deviation Risk |
Cost Multiplier Base = 1.0 (L/D ≤ 3) |
|
L/D ≤ 3 |
Standard Shallow Hole |
Single-pass solid carbide drilling |
External flood coolant |
±0.05 mm (IT11) |
Low (< 0.05 mm) |
1.0x |
|
3 < L/D ≤ 5 |
Medium Depth Hole |
Continuous drilling or single peck cycle |
Internal through-spindle coolant (20 bar) |
±0.08 mm (IT12) |
Moderate (0.05 to 0.10 mm) |
1.3x to 1.6x |
|
5 < L/D ≤ 10 |
High-Difficulty Deep Hole |
Parabolic flute drill + pilot pre-drill (1.5×D) |
High-pressure through-spindle coolant (40 to 70 bar) |
±0.12 mm (IT13) |
High (0.10 to 0.25 mm) |
2.2x to 3.5x |
|
L/D > 10 |
Extreme Deep Hole |
Single-lip gun drilling or deep-hole BTA drilling |
Dedicated gun drilling machine or high-precision CNC turning operations with guide bushings |
±0.15 mm (IT13 to IT14) |
Critical (> 0.30 mm drift at exit) |
5.0x to 10.0x |
Deep Hole Production Rules (L/D > 5):
· Incorporate Pilot Guides: When depth exceeds 5 times diameter, design entry faces perpendicular to the spindle axis within 0.5 degrees.
· Account for Exit Point Drift: Relax true position tolerances at the exit side of deep through-holes. If a hole requires an entry true position of Ø0.05 mm, the exit true position should allow at least Ø0.25 mm at an aspect ratio of 8:1.
· Avoid Stepped Deep Bores: Stepped internal cavities where the smaller diameter sits deep inside a larger bore cause chip recutting and step misalignments.
Process Selection Guide: Drilling vs. Reaming vs. Boring vs. Helical Milling
Selecting the correct manufacturing process requires balancing dimensional tolerance, geometric position capability, surface roughness, and production volume when evaluating drilling vs reaming vs boring CNC.

Before assigning precision tolerances, designers should evaluate standard aluminum machining tolerance standards to balance drawing expectations with real-world machine capability.
Dimensional Capability, ISO Fits (IT6–IT13) & Surface Roughness (Ra)
|
Machining Method |
Achievable ISO Tolerance Class |
Typical Dimensional Tolerance |
Surface Roughness (Ra) |
Centerline / True Position Capability |
Tool Setup & Cycle Time Index |
Primary Industrial Application |
|
Standard Twist Drilling |
IT11 to IT13 |
±0.100 mm to ±0.250 mm |
3.2 to 6.3 µm |
Low (Follows drill wander paths) |
1.0 (Fastest, single cycle) |
Clearance holes, bolt through-holes, pre-tap pilot holes |
|
Precision Reaming |
IT7 to IT8 |
±0.010 mm to ±0.020 mm (H7, H8) |
0.8 to 1.6 µm |
Dependent on pilot hole centerline |
1.8 (Requires pre-drill + ream pass) |
Dowel pin alignment holes, bearing retention pockets |
|
Single-Point Boring |
IT6 to IT7 |
±0.005 mm to ±0.010 mm |
0.4 to 0.8 µm |
High (Corrects previous axis runout) |
3.5 (Requires slow feed, fine-adjust head) |
Gearbox spindle bores, high-precision guide sleeves |
|
Helical Interpolation Milling |
IT9 to IT10 |
±0.025 mm to ±0.050 mm |
1.6 to 3.2 µm |
High (Governed by CNC encoder accuracy) |
2.5 (Continuous multi-axis toolpath) |
Non-standard diameters, counterbores, O-ring pockets on multi-axis CNC milling centers |
Standard Twist Drilling Mechanics
Standard drilling uses twin-lip rotary tools with continuous axial feed. The chisel edge at the center does not cut; it extrudes metal, generating 50% to 70% of total thrust force.
Expected CNC drilled hole tolerance results:
· Hole Entry: Expands +0.03 mm to +0.08 mm over tool nominal diameter due to initial contact runout.
· Hole Mid-Body: Matches tool diameter within +0.02 mm to +0.05 mm.
· Hole Bottom: Tapers inward or develops lobe geometry if chip packing occurs.
Precision Reaming Mechanics
Reaming is a sizing and finishing operation that removes a thin radial stock layer left by a pre-drilled pilot hole. The optimal radial material allowance for reaming is calculated as 0.05 mm plus 0.01 times the square root of the finished hole diameter. Reamers follow the existing center vector of the pre-drilled hole, correcting diameter, roundness, and surface finish, but cannot correct axis angular deflection or true position errors.
Single-Point Precision Boring
Boring utilizes an adjustable single-point cutting insert mounted to a rigid boring bar. The tool rotates while translating axially along the programmed spindle centerline. Because the rigid boring bar does not guide on the existing wall, it cuts away material eccentrically to correct drill wander, establishing exact true position within Ø0.01 mm and superior concentricity.
Helical Interpolation Milling
Helical milling moves a standard flat-end mill in a simultaneous 3-axis toolpath combining circular motion with continuous axial downfeed. The downfeed pitch per revolution should not exceed 15% of the cutter diameter, while the effective hole diameter spans from the cutter diameter up to twice the cutter diameter minus one millimeter. This method eliminates special drill inventory for non-standard diameters above 12 mm, though radial cutting pressure causes tool deflection that generates a slight taper (0.01 mm to 0.03 mm) in deeper cuts.
Four-Axis Engineering Decision Protocol for Hole Machining
1. Standard Clearance Holes: When tolerance is at or above ±0.1 mm, surface finish is Ra 3.2 µm or rougher, and standard diameters are used, select direct standard twist drilling for the lowest production cost.
2. Dowel Alignment Fits: When diameter tolerance is tight (±0.02 mm or ISO H7) and surface finish must be Ra 1.6 µm or smoother, but absolute position correction is not critical, select pre-drilling followed by precision reaming.
3. Critical Bearing Journals: When tolerance is within ±0.008 mm, surface finish must reach Ra 0.8 µm, and true position must be held within Ø0.02 mm, select pre-drilling, semi-finish milling, and single-point fine boring.
4. Large Non-Standard Cavities: When hole diameters exceed 16 mm, flat bottoms are required, or prototype batch volumes do not justify dedicated tooling, select helical interpolation milling.
CNC Threaded Hole Design Guidelines: Engagement Depth, Tooling & Inserts
Improper internal thread design causes tool breakage, thread stripping, and fastener failure during final torque assembly.

Thread Engagement Limits: The 1.5×D Pull-Out Strength Threshold
Specifying excessive thread engagement (such as threading an M6 fastener 20 mm deep into an aluminum housing) increases manufacturing risk without mechanical benefit. Fastener load distribution analysis demonstrates that thread engagement follows a non-linear shear curve:
· Thread Tooth 1 (First Engaged Tooth): Carries approximately 38% of the total axial tension load.
· Thread Tooth 2: Carries 25% of the load.
· Thread Tooth 3: Carries 18% of the load.
· Threads Beyond Tooth 6: Carry less than 5% of the combined load.
Optimal Thread Engagement Limits:
· Structural Steel, Cast Iron, High-Tensile Alloys: Thread engagement between 1.0 and 1.2 times nominal diameter.
· Aluminum Alloys, Magnesium, Brass: Thread engagement between 1.5 and 2.0 times nominal diameter.
· Engineering Plastics (PEEK, Delrin, POM): Thread engagement between 2.0 and 2.5 times nominal diameter.
Cut Tapping vs. Roll-Forming vs. Thread Milling Mechanics
For cut tapping, the pilot drill diameter equals the nominal thread diameter minus the thread pitch. For roll-form tapping, the required pilot drill diameter equals the nominal diameter minus 0.4375 times the thread pitch.
· Cut Tapping: Fluted tools that shear material away to produce chips. Required for cast irons, hardened steels above 35 HRC, and brittle non-ferrous alloys.
· Roll-Form Tapping: Non-cutting tools that cold-form metal fibers into thread profiles without creating chips. Yields 20% higher thread shear strength and eliminates chip packing in blind holes. Following precision aluminum CNC machining best practices makes roll-form tapping the preferred approach for ductile alloys like Al6061-T6.
· Thread Milling: CNC interpolation with a multi-tooth thread mill. Generates small chips, allows complete thread depth control within 1 pitch of the hole bottom, and allows the operator to remove a worn cutter without scrapping the workpiece.
Metric Thread Engineering Reference Matrix
The following reference table outlines parameters supporting our CNC threaded hole design guidelines for standard production hardware.
|
Thread Size (Standard Pitch) |
Cut Tap Pilot Drill Size (mm) |
Roll-Form Tap Pilot Drill Size (mm) |
Recommended Minimum Wall Thickness (t_wall) |
Min. Usable Thread Depth (1.5×D) |
Min. Pilot Hole Total Depth (Blind) |
|
M2 × 0.40 |
1.60 mm |
1.80 mm |
1.8 mm |
3.0 mm |
4.8 mm |
|
M3 × 0.50 |
2.50 mm |
2.80 mm |
2.5 mm |
4.5 mm |
6.8 mm |
|
M4 × 0.70 |
3.30 mm |
3.70 mm |
3.2 mm |
6.0 mm |
9.0 mm |
|
M5 × 0.80 |
4.20 mm |
4.60 mm |
4.0 mm |
7.5 mm |
11.0 mm |
|
M6 × 1.00 |
5.00 mm |
5.50 mm |
5.0 mm |
9.0 mm |
13.5 mm |
|
M8 × 1.25 |
6.80 mm |
7.40 mm |
6.5 mm |
12.0 mm |
17.5 mm |
|
M10 × 1.50 |
8.50 mm |
9.30 mm |
8.0 mm |
15.0 mm |
21.5 mm |
|
M12 × 1.75 |
10.20 mm |
11.20 mm |
10.0 mm |
18.0 mm |
26.0 mm |
Wire Thread Insert (Helicoil / STI) Pre-Tap Hole Tolerances
When soft metals face repeated disassembly, specify wire thread inserts. Always dimension the pre-tap hole to the dedicated STI (Screw Thread Insert) drill diameter specification, not the standard metric drill size. Include a 120° entry countersink with a diameter equal to the STI diameter plus 0.5 mm to prevent thread burring above the top mating face during insert driving.
Hole Spacing, Minimum Edge Distance & Cross-Hole Intersections
Holes do not exist in isolation. Their spatial proximity to outer component edges and adjacent internal cavities dictates internal stress states and geometric stability.

The 1.5×D Minimum Edge Distance Rule to Prevent Wall Bulging
When drilling near an unconstrained boundary, radial cutting forces generate shear stress that pushes material outward. Adhering to validated CNC hole spacing and edge distance limits avoids edge deformation during high-speed production runs. The distance from the hole center to the part edge must measure at least 1.5 times the hole diameter for solid billet stock, increasing to 2.0 to 2.5 times the diameter for thin-walled sheets and tubing.
Violating this rule leads to three distinct shop-floor defects:
· Edge Bulging: The external profile bows outward by 0.05 mm to 0.20 mm opposite the hole entry.
· Breakout during Tapping: Thread forming stresses tear through the thin web, ruining structural hold. Refer to our aluminum component design guidelines for safe edge distance ratios in light-alloy enclosures.
· Anodizing Burn: High electrical current density during anodizing concentrates on ultra-thin outer edges, burning the material.
Internal Web Spacing & Multi-Cavity Structural Integrity
The solid material bridge (webbing) separating two parallel holes must withstand both clamping forces and cutting thrust without vibration. The minimum web thickness between adjacent holes should measure at least 1.0 mm or half the diameter of the smaller hole, whichever is greater. For high-pressure hydraulic valve bodies operating above 200 bar, calculate web thickness based on material shear yield stress to avoid internal rupture between adjacent fluid channels.
Angled Surface Entry Spot-Facing & Cross-Hole Deburring Strategy
· Drilling into Angled Surfaces: If a drill strikes a surface angled greater than 5° from perpendicular, the chisel edge slips radially. This skids the tool off center and snaps solid carbide drills. Solution: Model a milled flat pad (spot face) perpendicular to the hole axis at the tool entry point.
· Intersecting Cross-Holes: When a drill breaks through into an existing internal cross-bore, cutting resistance drops to zero on one edge while the other edge remains engaged. This asymmetric load pulls the drill off axis, chipping the carbide margins. Dazao Shop Protocol: Program CNC feed rate reductions to 30% of nominal feed during cavity intersection, entering the breakthrough at reduced velocity and maintaining derated feed until the opposite wall is fully engaged. Manual deburring or thermal deburring (TEM) must be specified on drawings for internal intersections where loose burrs cause downstream hydraulic valve failure.
Dazao Shop-Floor DFM Checklist & The Cost-Tolerance Multiplier Curve
Use this 10-point checklist before releasing 2D production prints and 3D CAD files to reduce machining costs and cycle times.
The 10-Point Hole DFM Checklist
CAD Conical Point: Are all blind holes modeled with a standard 118° or 135° drill point rather than a flat bottom?
Standard Diameters: Are hole diameters aligned with standard metric tooling increments?
L/D Depth Ratio: Is the depth-to-diameter ratio kept under 5:1 wherever possible?
Thread Clearance: Does the blind pilot hole extend at least three pitches plus the drill point height past the required full thread depth?
Thread Depth Limit: Is usable thread engagement kept below 1.5 times diameter in steel or 2.0 times diameter in aluminum?
Edge Clearance: Is the center-to-edge distance greater than or equal to 1.5 times the hole diameter?
Web Thickness: Is the solid material separation between adjacent holes at least 1.0 mm or half the smaller hole diameter?
Angled Entry Spot Faces: Do holes on non-perpendicular surfaces feature a pre-milled flat entry face?
Post-Processing Drainage: Do blind holes undergoing anodizing or plating have a drain path to eliminate chemical entrapment?
Realistic Tolerancing: Are loose tolerances (±0.1 mm) assigned to clearance holes, reserving precision tolerances (within ±0.01 mm) strictly for dowel locations and bearing journals?
The Cost-Tolerance Multiplier Curve
|
Tolerance Range |
Process Strategy |
Relative Cost Per Hole |
|
±0.150 mm (IT13) |
High-Speed Carbide Drill |
1.0x (Baseline) |
|
±0.050 mm (IT10) |
Spot Drill + Precision Drill |
1.4x |
|
±0.015 mm (IT7) |
Drill + Ream (H7 Tooling) |
2.2x |
|
±0.005 mm (IT5 to IT6) |
Drill + Semi-Mill + Fine Bore |
4.8x to 7.5x |
Relaxing a non-critical hole tolerance from ±0.01 mm to ±0.10 mm removes the need for secondary reaming or boring cycles, cutting machining cycle time on high-hole-count parts by up to 40%.
Precision Hole Manufacturing Capabilities at Xiamen Dazao
Optimal hole design balances part function with standard shop-floor cutting dynamics. Specifying standard tooling diameters, keeping depth-to-diameter ratios under 5:1, avoiding non-functional flat-bottom blind holes, and factoring in pilot clearance for thread taps immediately reduces tool breakage, cycle times, and scrap rates.
At Xiamen Dazao Machinery, our facility operates over 60 high-precision 3-axis, 4-axis, and 5-axis CNC machining centers certified to ISO 9001:2015 and IATF 16949:2016. Our engineering team reviews every customer CAD model through an automated DFM protocol to detect hole design clashes before cutting metal.

FAQs
01.What is the depth-to-diameter limit before drilling costs increase exponentially?
02.Why do blind threaded holes break taps when modeled to full depth in CAD?
03.When should a drawing specify reaming instead of standard CNC drilling?
04.How does insufficient edge distance cause part failure during hole tapping?
05.Why do flat-bottom blind holes require secondary machining operations?
06.What causes white acid corrosion rings around blind holes after anodizing?